Tillverkare av stickat tyg sedan 2009 · Kina
Tillverkare av stickat tyg sedan 2009 · Kina

Key Sourcing Takeaways
Choosing a print method for custom knit fabric is not a finishing decision — it is a fabric specification decision. The wrong pairing between printing process and knit construction can mean uneven dye penetration, stiffened hand feel, or color inconsistency across production batches. Sourcing teams that lock in the print method before sampling avoid the most common reorder complications.
Unlike woven fabrics, knit constructions — including single jersey, interlock, and rib knit — have inherent elasticity from their loop-based structure. This creates two practical constraints on printing:
Beyond stretch, fiber content is the primary variable that determines which print method is technically viable. A 100% cotton jersey knit fabric and a 95% polyester performance knit require fundamentally different dye chemistries. Specifying the construction and fiber content up front is therefore a prerequisite — not a detail to confirm later in the sampling process.
GSM also plays a supporting role. Heavier-weight knit fabrics (depending on construction and finishing) may require adjusted ink viscosity or extended fixation time to ensure even penetration. These are variables that a knit fabric development team should account for at the print specification stage.
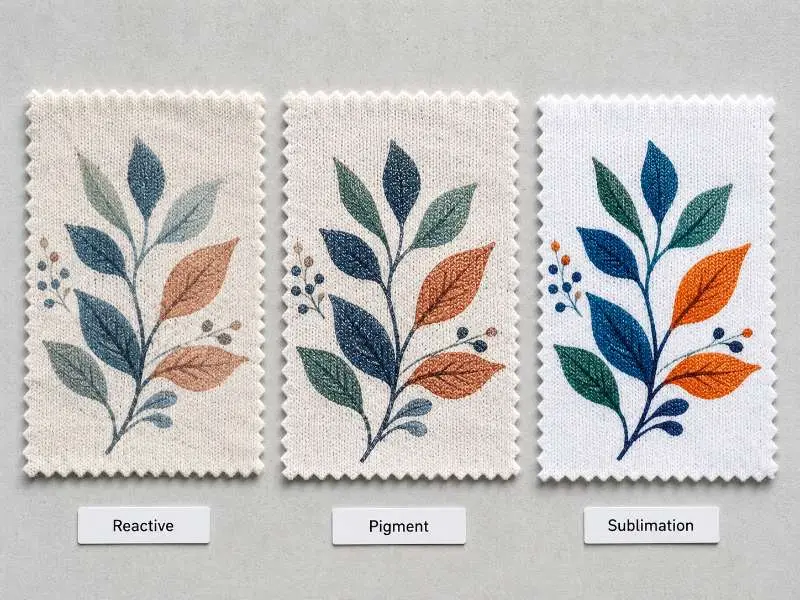
Reactive printing is the standard method for natural fiber knit constructions, particularly cotton and cotton-blend jerseys. The dye forms a covalent bond with cellulose fibers, which means it becomes chemically integrated into the fabric rather than sitting on the surface. For apparel brands producing T-shirts, casualwear, or loungewear on cotton-based knits, this results in:
In bulk production, the main sourcing consideration with reactive printing is batch consistency. Dye lots can vary between production runs due to differences in water chemistry, temperature, or fixation time. When placing bulk orders, buyers should request a specified acceptable shade band in writing — for example, a tolerance level measured against the approved sample — and confirm this before signing off on production. This is especially relevant for reorder programs where visual consistency across seasons is required.
Reactive printing is less effective on high-polyester substrates. Cotton content may need to be above a certain threshold (depending on construction) for reactive dyes to bond effectively. For blended knits, the actual cotton percentage in the blend should be confirmed before selecting this method.
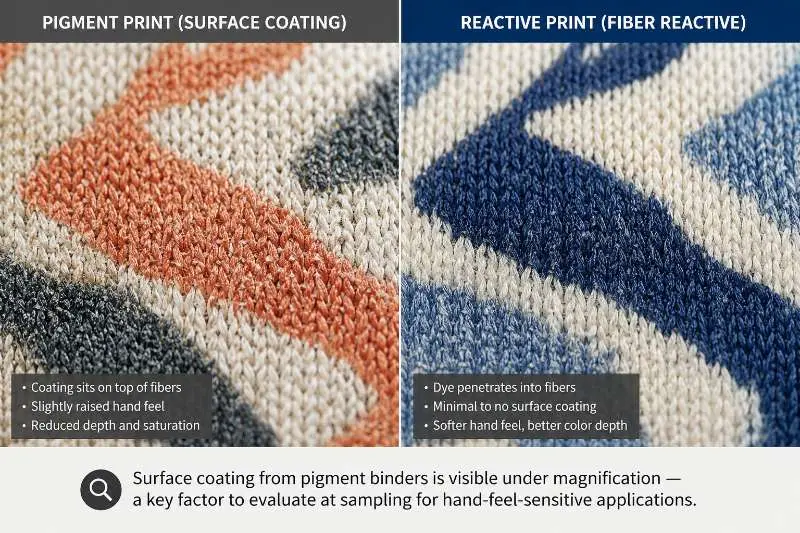
Pigment printing differs from reactive printing in a fundamental way: the colorant does not bond chemically with the fiber. Instead, a binder system adheres pigment particles to the fabric surface. This distinction has direct implications for sourcing decisions:
For bulk orders on knit fabrics, the critical verification point is wash fastness. Pigment prints that are not properly heat-set can show color degradation after multiple wash cycles. Buyers should request wash fastness test data — preferably to ISO 105-C06 or equivalent — for the specific fabric and ink combination before production approval.
Pigment printing is most suitable for straightforward graphic applications, limited colorways, or situations where substrate flexibility is more important than premium hand feel. For fine-gauge knits used in next-to-skin applications, the hand feel trade-off should be evaluated carefully at the sampling stage.
Dye sublimation converts solid dye into a gas under heat and pressure, embedding the colorant directly into polyester polymer chains. On custom knit fabric, this produces prints with exceptionally high color saturation, smooth gradients, and no perceptible hand feel change — because nothing is added to the fiber surface.
The hard constraint is fiber content. Sublimation dyes require a polyester substrate to bond with. In practice, this means:
For brands sourcing performance fabrics for training or sport applications, sublimation is often the preferred route for all-over print designs. The print withstands repeated washing and physical stress without cracking, provided the base fabric is correctly specified.
One practical sourcing note: sublimation is a pre-cut process applied to fabric rolls or finished panels before garment assembly. The heat application must be controlled precisely — inconsistent temperature across the width of a fabric roll can produce color variation in bulk. Verifying temperature consistency capability at the production stage is an appropriate quality checkpoint.
Regardless of which print method is selected for a custom knit fabric program, a structured sample approval process reduces production risk. The following checkpoints apply across all three methods:
If buyers require chemical safety verification for printed apparel fabrics, confirm whether the finished printed article can meet OEKO-TEX® Standard 100 requirements for the intended product class.
For brands managing custom dyeing for knit fabric alongside print programs, the same batch-control logic applies — recipe documentation and shade band management should be consistent across both dye and print development tracks to support reorder continuity.
Print method selection is also connected to the fabric development timeline. Reactive and pigment methods can generally be confirmed earlier in the sampling cycle. Sublimation may require the fabric base to be finalized first, given its strict polyester content requirement. Building this sequence into the sourcing calendar avoids delays at the lab-dip or strike-off stage.
Reactive dyes bond with cellulose fibers, so on a polyester-cotton blend, only the cotton portion accepts the dye. The result depends on the blend ratio — at higher polyester content, color depth will be noticeably reduced, and the undyed polyester may create a heathered effect. For blended custom knit fabric, the actual blend ratio should be confirmed before committing to reactive printing. An alternative is disperse-reactive combination printing, though this involves a more complex process.
MOQ varies depending on the print method and whether the fabric base is sourced from stock or developed to specification. For custom development programs, the general starting point is 200 kg per color for solid custom colors, and 1,000 kg for fully custom construction programs. Print-specific MOQs should be confirmed at the development briefing stage, as they depend on the production setup and the complexity of the colorway.
Reactive printing generally produces strong wash fastness when dye fixation is properly controlled — color bonded into the fiber is more resistant to laundering than surface-applied colorants. Pigment printing wash fastness depends heavily on binder quality and heat-setting parameters; ISO 105-C06 or an equivalent wash-fastness test is the clearer way to verify this before bulk approval. If chemical safety certification is required, confirm whether the printed article can meet OEKO-TEX® Standard 100 requirements for the intended product class.
Runtang Textile manufactures custom knit fabrics across a full range of constructions and fiber combinations, with print development support available through the sampling process. Request a sample or get a quote to start your print sourcing process.
 Branschinsikter
4 vanliga typer av klädtyger
LÄS MER Insikter från tillverkaren
Efterbehandling av stickade tyger för konfektion: ruggning, peaching, mercerisering och tvätt – vad varje steg ger i storvolym
LÄS MER Tyg
Velourtrikå: ett lyxigt val för vardagskomfort
LÄS MER Inköpsguide
Stickat tyg för underkläder: vad inköpare behöver veta om mjukhet, stretch och säkerhet vid hudkontakt
LÄS MER Insikter från tillverkaren
Reklamationer på defekter i stickade tyger: dokumentation, inspektionsrapporter och arbetsflöde för hantering
LÄS MER